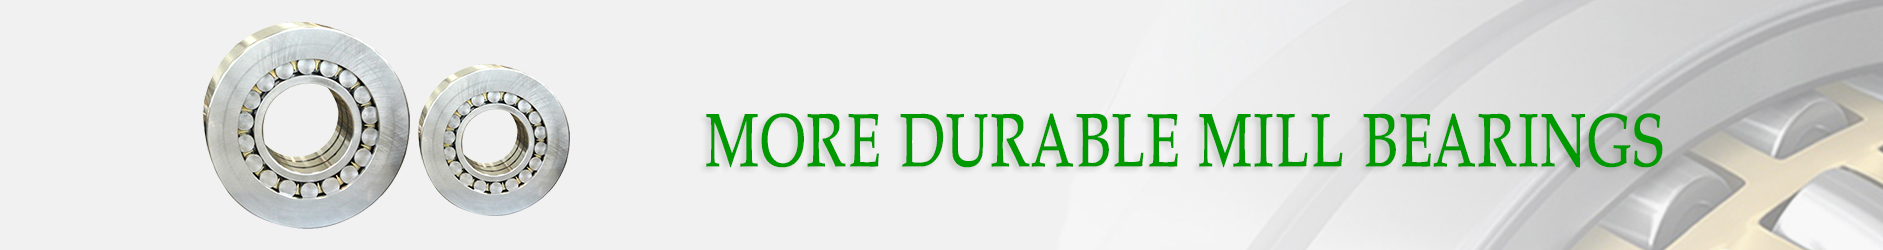
In the main production line of the wide and thick plate workshop of a large steel plant, the export frame rollers of the rolling machine are equipped with double-row self-aligning roller bearings. These bearings have the characteristics of bidirectional bearing capacity and automatic self-alignment, and can adapt to situations such as slight bending of the shaft body and installation alignment deviations. The designed service life is 8,000 hours. They mainly bear the guiding and conveying loads during the wide and thick plate rolling process and are the core component ensuring the flatness of the rolled plates.
The operating side bearing of the first frame roller at the exit of this rolling mill frequently malfunctioned. The newly replaced original bearings broke completely within just one month of operation. The equipment experienced severe vibrations and abnormal noises, the frame roller's rotation became stuck, which directly caused the deviation of the wide and thick plate rolling and defects in the plate surface. The production line was forced to stop urgently. This fault was a repetitive one, and similar breakage problems of this kind occurred consecutively for three times in a short period of time, seriously affecting the continuous production of the production line. The operating side bearing of the first frame roller at the exit of this rolling mill frequently malfunctioned. The newly replaced original bearings broke completely within just one month of operation. The equipment experienced severe vibrations and abnormal noises, the frame roller's rotation became stuck, which directly caused the deviation of the wide and thick plate rolling and defects in the plate surface. The production line was forced to stop urgently. This fault was a repetitive one, and similar breakage problems of this kind occurred consecutively for three times in a short period of time, seriously affecting the continuous production of the production line.
After technicians disassembled the failed bearing and inspected the equipment's operating conditions, they identified that the core fault causes were as follows:
1.Installation alignment deviation exceeded the standard: The roller bearing housing of the frame had slight deformation during long-term operation. During routine maintenance, the coaxiality was not accurately calibrated, causing the bearing to continuously bear abnormal eccentric loads during operation. Local stress concentration occurred in the outer ring, far exceeding the rated load limit. The compensatory structure that could previously accommodate minor deviations completely failed due to excessive deviation.
2. Frequent impact loads: During the rolling process of thick plates, there were fluctuations in plate thickness and significant impacts during steel biting. The frame roller continuously endured intermittent impact loads. The fatigue damage of the bearing outer ring accumulated continuously, accelerating the initiation and expansion of cracks.
3. Poor lubrication conditions: There was slight blockage in the equipment's lubrication pipeline, and the supply of lubricating oil was uneven. Local dry friction occurred between the rolling elements of the bearing and the outer raceway, resulting in high-temperature burns, reducing the fatigue strength of the bearing metal, and ultimately causing brittle fracture of the outer ring.
1. Precisely adjust the installation accuracy of the bearing housing. Use a dial indicator to calibrate the coaxiality of the frame rollers, and control the installation deviation within 0.03mm, completely eliminating the eccentric load problem.
2. Optimize the rolling process parameters, adjust the steel biting speed of the steel plate, and reduce the instantaneous impact load; for plates with thickness fluctuations, add a buffering rolling program to reduce equipment impact loss.
3. Fully unclog the lubrication pipeline, replace the high-precision filter element, formulate a fixed-point and fixed-time lubrication standard for the bearings, and check the loss and contamination of the lubricating grease during each maintenance to ensure the full coverage of the oil film on the raceway.
4. Establish a special inspection mechanism, focus on monitoring the vibration and temperature data of the frame rollers, and predict potential fatigue damage risks in advance.
After the rectification was completed, no more breakage faults occurred at this position bearing. The average service life of the bearing returned to over 8,000 hours as per the design standard, completely resolving the repetitive downtime issues. Monthly unplanned downtime was reduced by 4 hours, effectively lowering the defective rate of the plates, and ensuring the stable and efficient operation of the wide plate production line.
WeChat official account
Scan and focus on us
Address:24th floor, Tianjin Property Building, 590 Shengan Road, Huishan District, Wuxi City, Jiangsu Province Tel : 13861477666 E-mail : jsdmdbearing@163.com ©2020 江苏帝蒙德轴承有限公司. 版权所有 苏ICP备16008043号-4